 Deutsch
 Français
 Italiano
 Español
 Shqip
 Српски
 Български
 Română
 Türkçe
In production at asphalt plants in Greece
iAsphalt: Every tonne of asphalt mix with the right bitumen content and the right temperature.
iAsphalt controls cold-feed dosing, dryer drum and burner, screen and hot bins, bitumen and filler scales, mixer and filters on any asphalt plant. Installed or upgraded in 1 day, with the tonnes and bitumen content of every production on your phone.

iAsphalt is built on iOLABS Live Control: we write the controller code ourselves, connect to any PLC, and the operator holds the plant in their hand, on web, tablet or desktop. The shared capabilities (recipes, interlocks, operating modes, calibration, users, backups) are described there once. This page covers what is specific to asphalt.
What you gain
-
The mix design's bitumen content, in the mixer
The bitumen scale doses with high-accuracy load cells and in-flight correction, batch by batch. Deviation per material is logged, so the lab sample holds no surprises.
-
Live control in your hand
One live picture of the plant on web, tablet and desktop. The operator commands from wherever they stand, the owner sees the same screen from the office. One system from the controller code to the cloud.
-
Aggregate and bitumen temperature under control
Thermocouples at the dryer outlet, in the hot bins, in the bitumen tanks and in the oil circuit. The burner is regulated so the mix leaves at the temperature the recipe asks for, not 20 degrees higher just to be safe.
-
Dryer and burner with less fuel
Automatic ignition, control of fuel-oil or diesel injection and circulation, fuel temperature monitoring. The flame follows the material flow instead of burning at maximum all day.
-
Hot bins and screen without overflow
Levels per fraction, overflow discharge, current monitoring of screen and elevator. The operator sees where each fraction goes before the wrong bin fills up.
-
Installed in 1 day
Panel and software are prepared in our workshop. On site we do the changeover, test batches and operator training. The same applies to mobile plants that move from project to project.
-
Switch cold-feed bins without stopping
When a cold-feed bin runs empty the operator pulls the same fraction from another with one tap, inside automatic production.
-
Filters and dust working together
Control of baghouse or hydrocyclone, dust screws and filler. Reclaimed dust returns to the recipe as a dosed material, not as an unpredictable addition.
-
Compliant with international asphalt production standards
Theoretical and actual quantities per fraction, bitumen content, temperatures and mixing time recorded per batch, ready for quality control and for the project owner.
-
Tonnes and bitumen content on your phone
Every production uploads automatically to the iOLABS Automations Cloud: tonnes per day, recipe and customer, real versus theoretical bitumen content, consumption, batch duration, alerts.
-
Delivery notes and accounting, connected
Productions feed iAsphalt DMS for delivery notes with myDATA and any accounting package or ERP.
How it works


-
01
The panel
An iOLABS IP54 panel with main switch, power relays, dosing inverters, motor cabling and a modern Ethernet controller. It replaces the old panel or is fitted onto it, with plug & play wiring on mobile plants.
-
02
The signals
Load cells of the aggregate, bitumen and filler scales, PT100 thermocouples, level sensors, safety limit switches and ammeters reach the PLC. iAsphalt reads them hundreds of times per second.
-
03
Cold feed and dryer
Cold feeders dose the recipe's fraction ratios through inverters. The drum dries and heats, the burner is regulated by the outlet temperature, the elevator lifts the material to the screen.
-
04
Screen, hot bins, weighing
The screen separates fractions into the hot bins. The aggregate scale weighs cumulatively per fraction, the filler scale and the heated bitumen scale dose in parallel, with free-fall correction on every scale.
-
05
The mixer
Dry mixing, bitumen spray from the nozzles, wet mixing with times per recipe, discharge to the truck or to the storage silo. Mixer current monitoring protects against overload.
-
06
The record and the cloud
Every batch is stored with theoretical and actual weights, temperatures, time and operator, and uploads automatically to the iOLABS Automations Cloud within seconds.
Modules
-
Cold-feed dosing
Inverter-driven feeders, ratios per recipe, vibrators, automatic bin switching, collecting belt control.
-
Dryer and burner
Automatic ignition, fuel injection and circulation, pre-heater, aggregate outlet temperature, safety limit switches, flame regulation.
-
Screen and hot bins
Levels per fraction, overflow discharge, current monitoring of screen, elevator and screws.
-
Aggregate, filler and bitumen weighing
Cumulative weighing per fraction, filler scale, heated double-wall bitumen scale discharging to nozzles or pump.
-
Bitumen tanks and oil heater
Tank and oil-circuit temperatures, tank burners, safety limit switches, tank selection per recipe.
-
Mixer and discharge
Dry and wet mixing, bitumen spray, times per recipe, discharge to truck or silo, current monitoring.
-
Filters and dust
Baghouse or hydrocyclone, dust screws, dust return to the recipe, filter motor monitoring.
-
Productions and reports
Batch printout, consumption of aggregates, bitumen, filler and fuel, deviations, export to accounting and to iAsphalt DMS.
-
iOLABS Automation Core
Recipes, four operating modes, two-step calibration, self-tuning, maintenance, tablet, users, backups, multilingual.
Learn more
Specifications
| Controllers | Siemens, Beckhoff and any modern PLC or controller, over standard industrial protocols (Modbus, Profinet, OPC UA). Controller code written by iOLABS. |
|---|---|
| Control interface | iOLABS Live Control: live screens on web, tablet and desktop; SCADA/HMI functions built in |
| Communication | Wired network, Wi-Fi for tablet, secure remote support |
| Architecture | iOLABS Live Control with a secure production database; LEMS (Less Electronics More Stability), ATS (Auto Tuning System), SCS (Self Care System) |
| Scales | Hot aggregates (cumulative per fraction), filler, bitumen (heated, double wall), optionally reclaimed material |
|---|---|
| Sampling | Thousands of samples per second, digital filtering, automatic free-fall correction |
| Temperatures | iOLABS PT100 / thermocouples at dryer outlet, hot bins, bitumen tanks, oil circuit, fuel |
| Calibration | 2 steps by the operator, values logged |
| Plant types | Mobile and stationary batch asphalt plants, any capacity |
|---|---|
| Cold feeders | Inverter control, unlimited bins |
| Panel | Metal IP54, main switch, power relays, inverters, cabling, controller with wired and wireless communication |
| Operation | Automatic, semi-automatic, manual, maintenance |
|---|---|
| Users | Roles and permissions, action log, automatic and manual backups |
| Languages | Greek, English, extensible |
| Integrations | iAsphalt DMS, iBridge, any accounting package/ERP, iOLABS Automations Cloud |
| Compliance | International asphalt production standards |
Media


Integrations
References
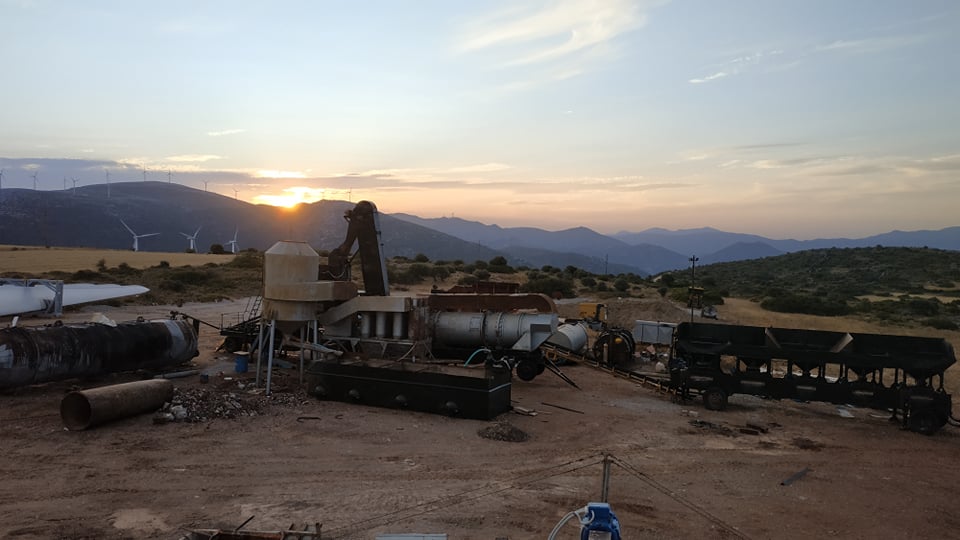
Greece, GR · 2020
Full reconstruction of a mobile asphalt plant and iAsphalt for TEVAR S.A.
Mechanical and electrical reconstruction of a TEVAR S.A. mobile asphalt plant with new iAsphalt automation. Set up and producing in 1–2 days.
Learn more Full reconstruction of a mobile asphalt plant and iAsphalt for TEVAR S.A.

FAQ
Will iAsphalt fit my asphalt plant?
How long will the plant be out of production?
Does it control the dryer and the burner as well?
How is the bitumen content guaranteed?
Can the operator calibrate the scales alone?
What happens if a thermocouple or sensor fails mid-production?
Can I see production on my phone?
Is there a demo?
Help
- Bitumen temperature and the bitumen scaleBitumen weighs correctly only when it flows correctly, and it flows correctly only at the right temperature. iAsphalt monitors the temperature in the tanks, the supply line and the scale, and does not allow dosing outside the limits.
- Hot bins, screen and alarmsOn an asphalt plant the hot aggregates go from the dryer drum to the elevator, the screen and the hot bins, from where they are weighed per fraction. iAsphalt monitors every stage and warns you before a full or empty fraction stops production.
- Asphalt mix recipes and bitumen percentageA recipe in iAsphalt defines the aggregate fractions, the filler, the bitumen percentage and the mixing times. The system weighs every component per batch, records theoretical and actual quantities and computes the real bitumen percentage, the number that matters to quality control and to the customer.
Works with

iAsphalt DMS
Online delivery notes for asphalt and recycled materials, with QR and MARK on myDATA, daily schedule, return notes and accounting integration.
Learn more iAsphalt DMS
iBridge
Weighbridge management: unattended weighing with RFID, first/second weighing tickets, traffic lights and barriers, digital delivery notes with myDATA.
Learn more iBridge
iLoading
Automatic pre-loading of aggregate bins: the operator picks a bin, the system opens belts, diverters and gates in the right order and stops when it is full.
Learn more iLoading
iFleet
Live fleet view, routes, consumption and driver sheets. With a GPS tracker in the vehicle or a tablet running the iFleet Tracker app, no extra hardware.
Learn more iFleet- Service

Bitumen scales
iOLABS-built bitumen scales: double-wall vessel with hot-oil circulation, optional built-in electric oil heater, high-precision load cells.
Learn more Bitumen scales - Service
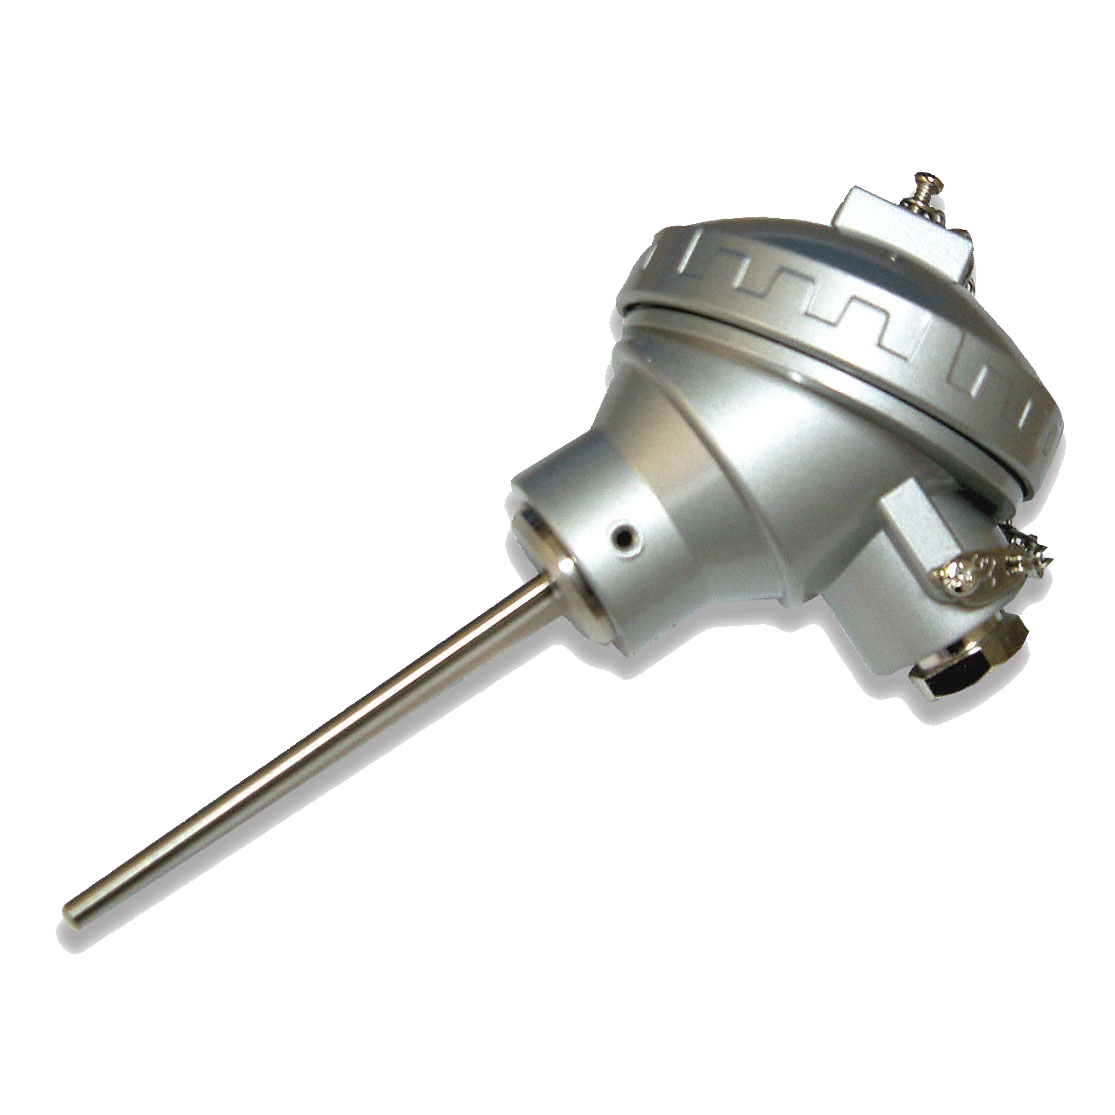
Thermocouples & temperature sensors
Thermocouples, PT100 resistance thermometers and temperature sensors made by iOLABS, in any diameter, length and thread, for any industrial application.
Learn more Thermocouples & temperature sensors


See iAsphalt on your own plant.
One visit or video call with our engineer is enough to know what is needed and how long it takes.